Inside a Leading China SLA 3D Printer Factory for High-Precision Prototyping
2026-11-02
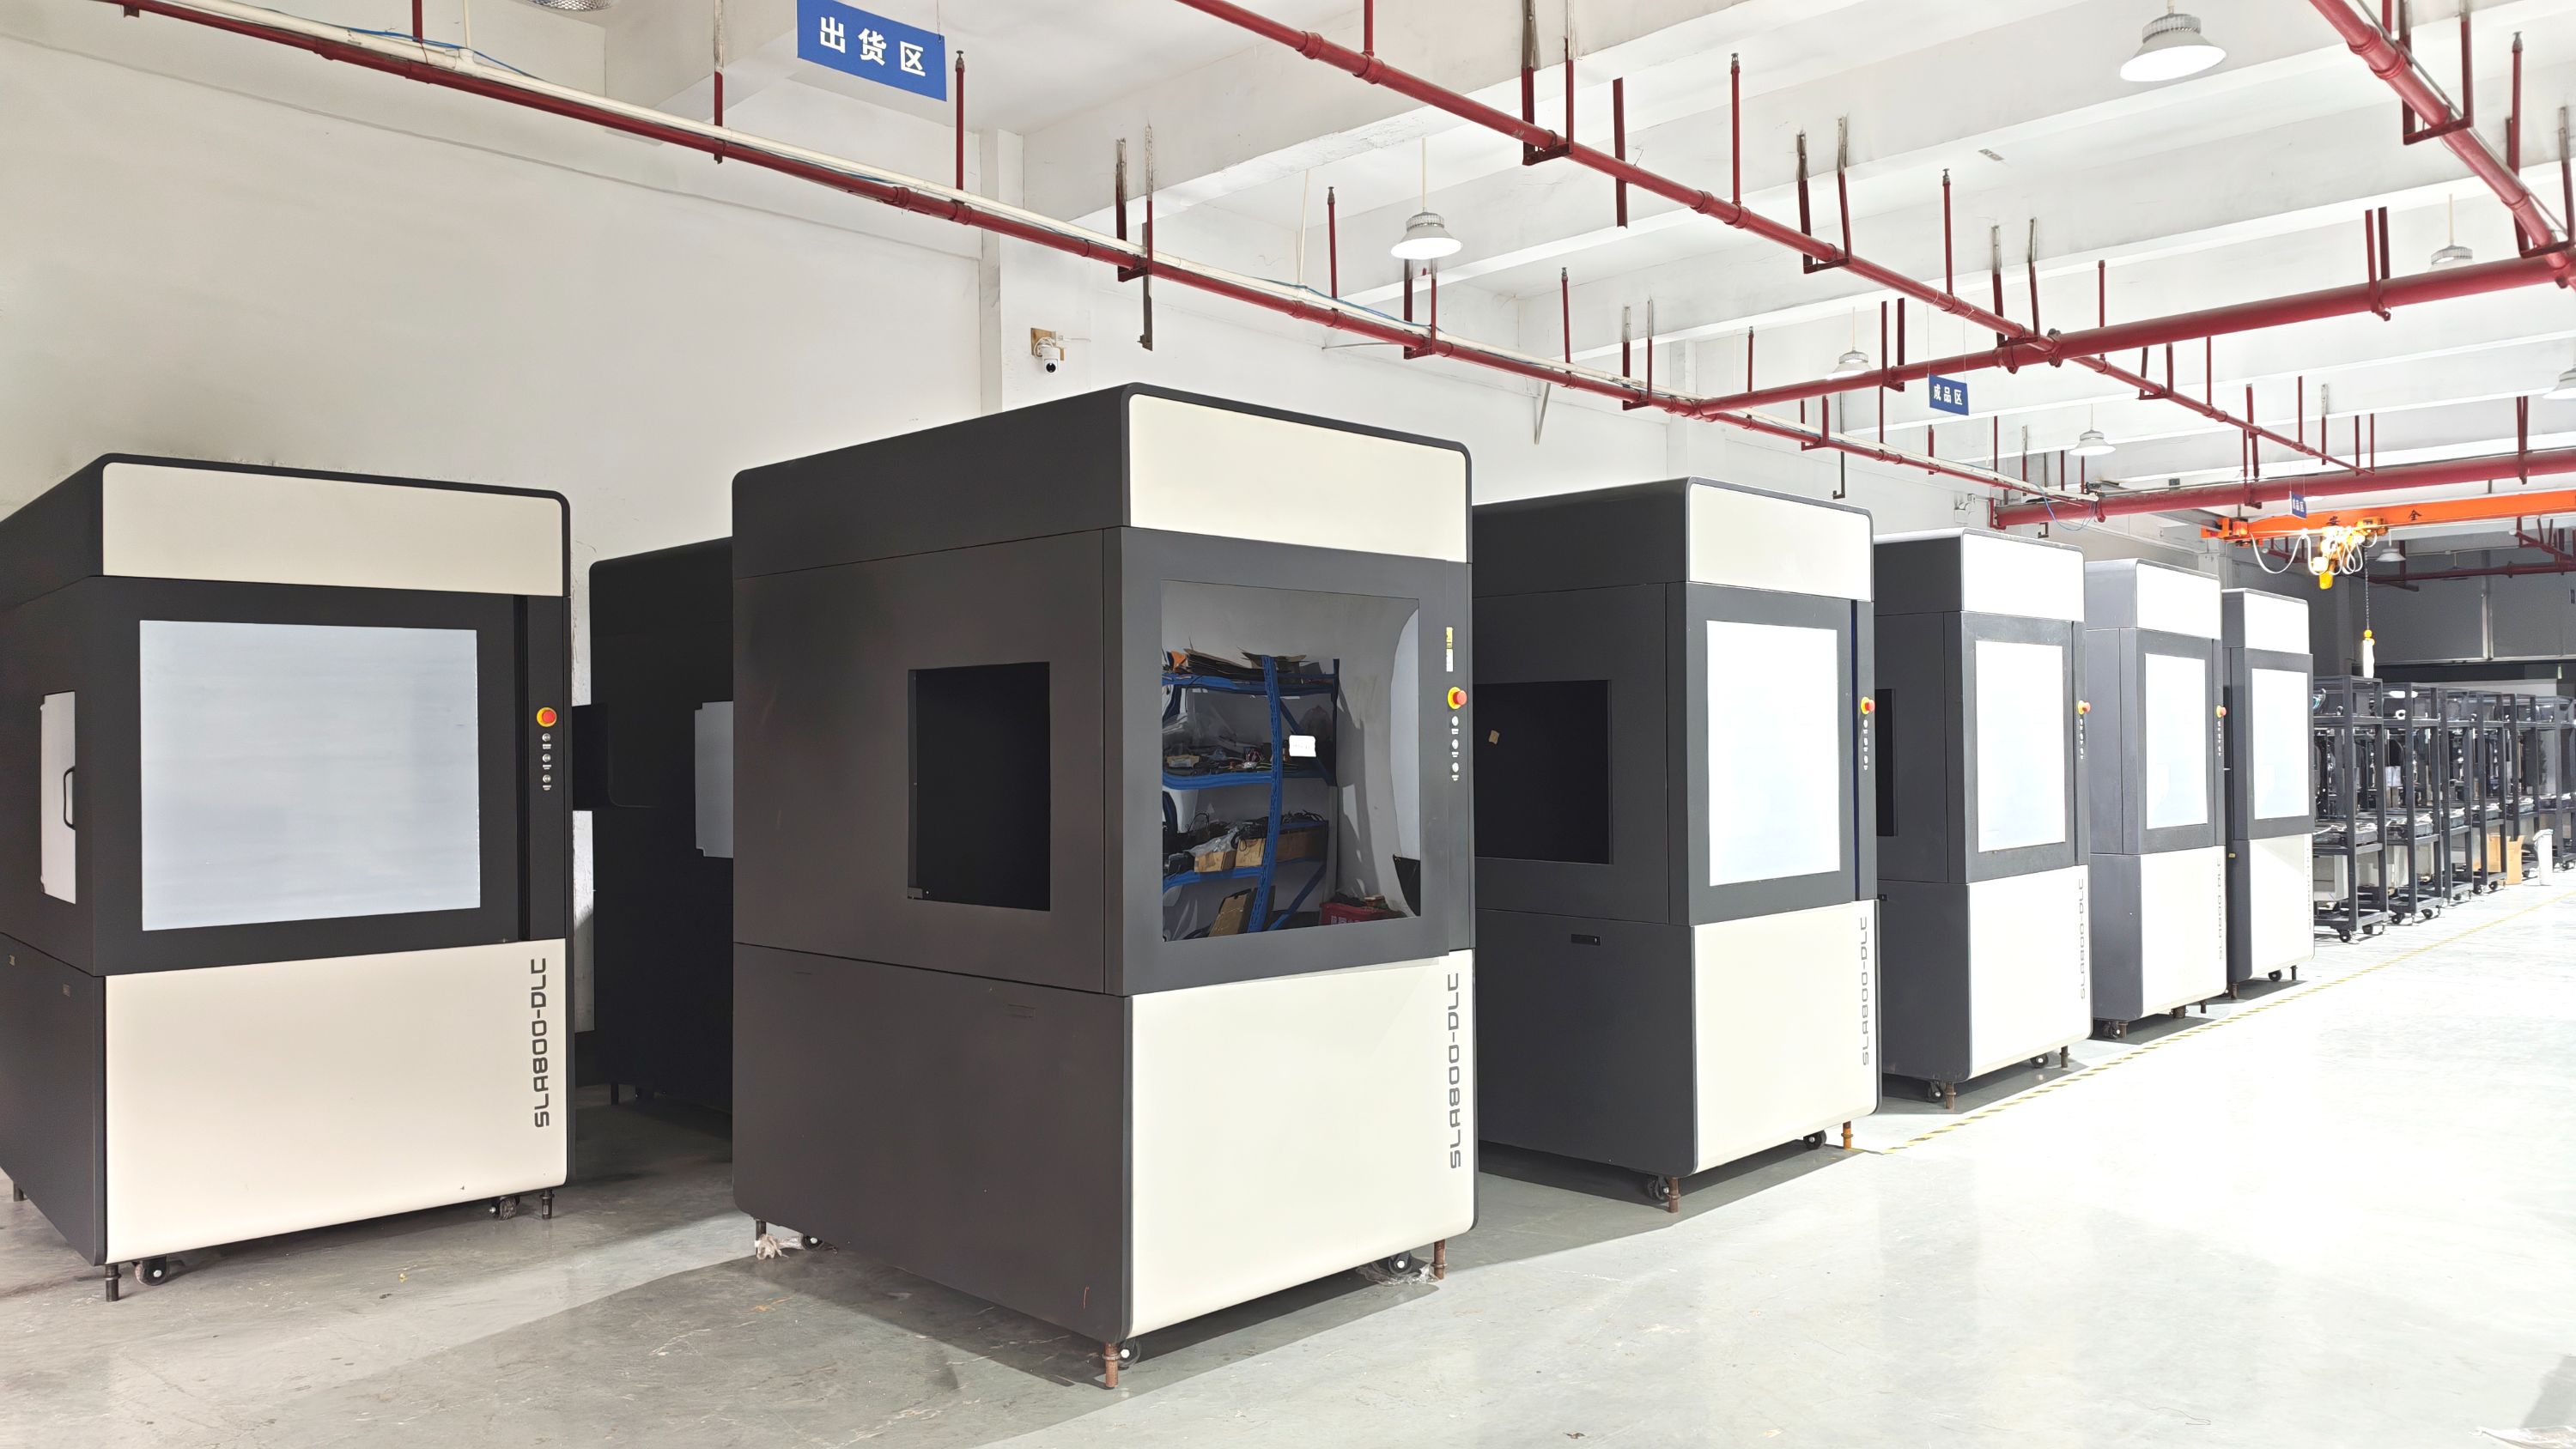
When you walk through the doors of ProtoMat's production facility, the first thing that hits you is the sheer scale—rows of SLA 3D printers calibrated not just for speed, but for the kind of high-precision prototyping that most factories only promise. This isn't a showroom; it's where tolerances are measured in microns and every build plate carries a client's do-or-die deadline. In this behind-the-scenes look, we go inside the workflows, materials, and quality checks that make ProtoMat a quiet powerhouse in China's additive manufacturing scene.
Where a Vat of Resin Becomes a Working Prototype Overnight
The digital file is queued just before midnight. Inside the printer, a vat of liquid resin sits still, waiting. Ultraviolet light traces the first layer across the build platform, and the resin hardens in precise patterns. Over the next several hours, the process repeats—layer after layer, each as thin as a human hair. By dawn, a fully solid part has emerged from the liquid, its geometry locked in place.
There is no need to wait for tooling or outsource to a machine shop. This is the quiet power of resin-based rapid prototyping: a design created on a screen becomes a physical object while the office sleeps. The next morning, the part is rinsed in solvent, cured under UV lamps, and fitted into an assembly. If it fails, the file is tweaked and the vat does its work again the following night. That overnight turnaround has collapsed weeks of traditional iteration into a single sleep cycle.
The Daily Calibration Checks That Keep Laser Paths Honest
Most labs run a quick beam alignment against reference targets before the first real measurement. A few microns of drift from thermal expansion or a bumped mirror can send the focal spot wandering, and nobody wants to discover that halfway through a batch run. The check itself is simple: fire a low-power pulse, compare the centroid on a CCD or position-sensing detector, and adjust the last steering mirror if the offset exceeds tolerance.
Daily records also catch slower degradation that a single pass won't reveal. Over a week, a gradual shift in output power or a widening beam profile often points to contamination on a window or slight loosening of a kinematic mount. By logging the numbers before routine work begins, technicians can separate normal variation from wear that needs scheduled maintenance, instead of chasing ghosts after a failed experiment.
Why Operators Here Watch the First Layers Like a Hawk
The first layers of any system carry an outsized burden. They set the tone for everything that follows, and operators here know that a minor slip at the start can cascade into hours of confusion later. That's why they hover over those initial outputs, comparing every value against expected baselines before letting the process run further. It's not paranoia—it's hard-won experience from too many late nights spent untangling errors that could have been caught in the first five minutes.
There's also a practical reason: the first layers are where configuration mistakes love to hide. A swapped parameter, an off-by-one index, or a silently defaulted setting rarely announces itself loudly. By the time the middle layers churn through the data, the problem has been amplified and buried under layers of legitimate computation. Watching the early stages closely lets operators spot the anomaly while it's still small enough to fix without a full restart.
And then there's the rhythm of the work itself. Operators develop an instinct for what a healthy first layer looks like—the way the numbers settle, the pattern of memory allocation, the timing of the first checkpoints. When that rhythm breaks, even slightly, they notice before the dashboards do. It's a kind of attention that can't be automated away, because it's built on thousands of hours of seeing both the clean runs and the messy ones.
From Isopropyl Baths to UV Curing Racks, the Hidden Post-Processing Line
The moment a print lifts off the build plate, it's still sticky with uncured resin. Sliding it into an isopropyl bath isn't just a quick rinse—it's a careful dance of agitation and timing. Too short and the surface stays tacky; too long and fine details start to soften. Most people never see this part of the workflow, but it's where dimensional accuracy either holds or quietly slips away.
After the bath, the model drips for a while on a wire rack, but that's only half the story. The real transformation happens under UV light, on shelves that look deceptively simple. A curing rack with consistent 405nm exposure turns a fragile, semi-cured shell into a solid part. Without proper rotation and spacing, shadows leave soft spots, and those soft spots become warps days later.
Hidden post-processing lines are rarely photographed for product pages, yet they decide whether a resin print survives its first week on a desk. From the temperature of the isopropyl to the distance between UV tubes, every variable belongs to a routine that feels more like lab work than 3D printing. And once you treat it that way, the difference shows up in edges that stay crisp and surfaces that don't go cloudy.
How Tight Tolerances Survive When the Order Is Only Three Parts
When a machine shop gets a call for three parts with tolerances measured in microns, most will quote a price that makes the customer flinch. The usual playbook assumes that tight tolerance work only makes sense at volume, where setup time and tooling wear can be spread across thousands of cycles. But for a three-piece order, there's no volume to hide behind. Every first cut has to be right, every measurement has to hold, and every scrapped part is a third of the job gone. The shops that survive this niche don't rely on luck. They survive because they've built their entire process around the idea that a single part and a thousand-part run deserve the same level of attention.
One key is refusing to treat setup as a cost center. In low-volume tight tolerance work, setup time dwarfs machining time. A shop that takes three hours to dial in a fixture, indicate a vice to within a tenth, and warm up a spindle before the first chip flies isn't wasting time—they're buying certainty. They use pre-machined soft jaws, temperature-controlled inspection areas, and they measure the first part like it's the last part they'll ever make. If a tool deflects by a few microns on part one, that's not a lesson learned for the next batch; it's a failure on the only batch. So they compensate, adjust, and re-cut until the part prints dead center of the tolerance band.
There's also a quiet stubbornness about material selection and process order. With only three parts, there's no chance to tweak speeds and feeds between pieces. The machinist has to know, from experience, how 17-4 stainless will move after roughing, how much a thin wall will spring back after the clamps are released, and whether to rough everything first or finish each feature in a single setup. Some shops will even run an identical test part in aluminum just to validate tool paths, even though aluminum behaves nothing like the final material. It sounds wasteful, but when the alternative is scrapping a $400 chunk of hardened tool steel on the second cut, a $20 test blank is the cheapest insurance in the world. That mindset—spending small to protect the only three shots you get—is what keeps tight tolerances alive when the order is barely enough to fill a shoebox.
What the Final Inspection Bench Reveals About Surface Finish and Detail
A well-lit final inspection bench does more than confirm a part meets basic dimensions—it exposes the story of every tool path, sanding pass, and polish step. Under raking light, subtle waves, micro-scratches, and uneven gloss become impossible to ignore. The bench is where surface finish stops being a spec sheet number and turns into something you can run a fingertip over.
Detail verification at this stage hinges on contrast and reference. Operators often keep a set of approved master samples nearby, not to compare measurements but to compare character. A tiny radius overlooked in CAD, a parting line left proud, or a grain mismatch on veneer all surface here. The bench rewards patience and punishes rushed upstream work.
Perhaps more revealing is what the bench teaches about process stability. When the same defect keeps appearing at the same spot under the same light, it points to a fixture issue or tool wear, not operator error. That feedback loop transforms the final inspection bench from a gate into a diagnostic tool.
FAQ
The biggest difference is how tightly they control the laser calibration and build chamber temperature. Most shops rely on default settings, but here technicians run a full beam profile check every morning and adjust the galvo mirrors before production starts. That alone reduces dimensional drift on thin features by a noticeable margin.
It starts with resin temperature. They keep the vat at a stable 28°C and let the machine idle for 20 minutes before the first print. Layer height is typically 50 microns for cosmetic parts and 25 microns for fine detail work. After each build, the platform is checked against a reference jig, not just a visual scan.
A lot of medical device teams use it for housing prototypes and surgical guides because the tolerances are predictable. Consumer electronics brands come for snap-fit enclosures. Automotive suppliers often request clear resin parts for flow visualization. The common thread is that they need repeatability across multiple iterations.
You send a STEP or STL file, and within a few hours an engineer reviews it for unsupported overhangs and wall thickness. They propose orientation and support placement before printing. Once approved, the part goes into a batch with similar resin types. After printing, it gets two-stage IPA washing, UV curing, and support removal by hand under magnification.
Every part is measured on a CMM for critical dimensions, and the surface is inspected under a ring light for pinholes or layer lines. If the customer has specified a tolerance band, they check three points on each axis. Parts that fail are reprinted immediately rather than shipped with a waiver.
The key is custom support scripting. They don't rely on the slicer's default auto-support. For walls under 0.8 mm, they add a temporary rib structure that gets sanded off later. Lattices are printed at a slower scan speed with reduced laser power to avoid overcuring. It's more manual, but the success rate is much higher.
They stock about a dozen resins, including ABS-like, high-temp, flexible, and castable. The vat is filtered after every print to remove cured particles, and leftover resin from the build platform is drained back into sealed containers. Expired resin is never mixed with fresh batches; it gets sent for recycling.
They recently switched to a dual-laser system on two of the larger machines, which cut average build time by roughly 40%. They also started batching parts by resin family instead of customer order, so the machines stay warm longer and calibration overhead drops. That has shortened standard turnaround from five days to three for most orders.
Conclusion
Stepping onto the floor of this leading SLA 3D printer factory, the first thing you notice is how a vat of liquid resin can turn into a working prototype by morning. Technicians run through daily calibration checks on every laser path, making sure the beam stays true across the build platform. It’s not flashy work, but it’s what lets a customer email a file at 4 p.m. and hold a finished part at 9 a.m. the next day. Operators hover near the machines during those first few layers, watching for any sign of peel force trouble or uneven curing—a habit born from years of learning that the foundation decides everything.
After the build, parts move through a hidden post-processing line: isopropyl baths to strip uncured resin, then UV curing racks to lock in mechanical properties. Even when an order is only three parts, tight tolerances survive because the process is treated like a production run, not a one-off experiment. The final inspection bench is where surface finish and fine details get scrutinized under angled light and magnification. Small layer lines, crisp edges, tiny embossed text—nothing slips through. That combination of overnight speed, obsessive calibration, and honest post-processing is what keeps this factory ahead in high-precision prototyping.
Contact Us
Contact Person: Joe
Email: [email protected]
Tel/WhatsApp: +8613799507208
Website: https://www.3dprotomat.com/